Dial indicators bulk: why zero-reset errors increase after repeated shock loading
Author
Date Published
Reading Time
Repeated shock loading on dial indicators bulk units—common in high-vibration manufacturing, calibration labs, and field metrology—introduces cumulative zero-reset errors that compromise measurement integrity. This issue directly impacts reliability-critical applications across Instruments & Measurement, Mechanical Components & Metallurgy, and Environmental Test Chambers. As procurement professionals and EPC engineers source precision tools like digital calipers manufacturer-grade devices or portable hardness testers, understanding root-cause failure modes becomes essential—not just for compliance (ISO/IEC 17025), but for long-term TCO control. Global Industrial Core investigates the physics of mechanical hysteresis, wear dynamics, and recalibration drift—backed by metrology lab validation.
Why repeated shock loading degrades zero-reset accuracy in bulk dial indicators
Dial indicators—especially those procured in bulk for production line deployment or calibration facility redundancy—are subject to microstructural fatigue when exposed to repetitive mechanical shocks. These shocks occur during transport, mounting on vibrating machine bases, or accidental drops during field use. Unlike single-unit metrology instruments used under controlled lab conditions, bulk-distributed units often lack individual shock-absorbing packaging and undergo 3–5 handling cycles before final installation.
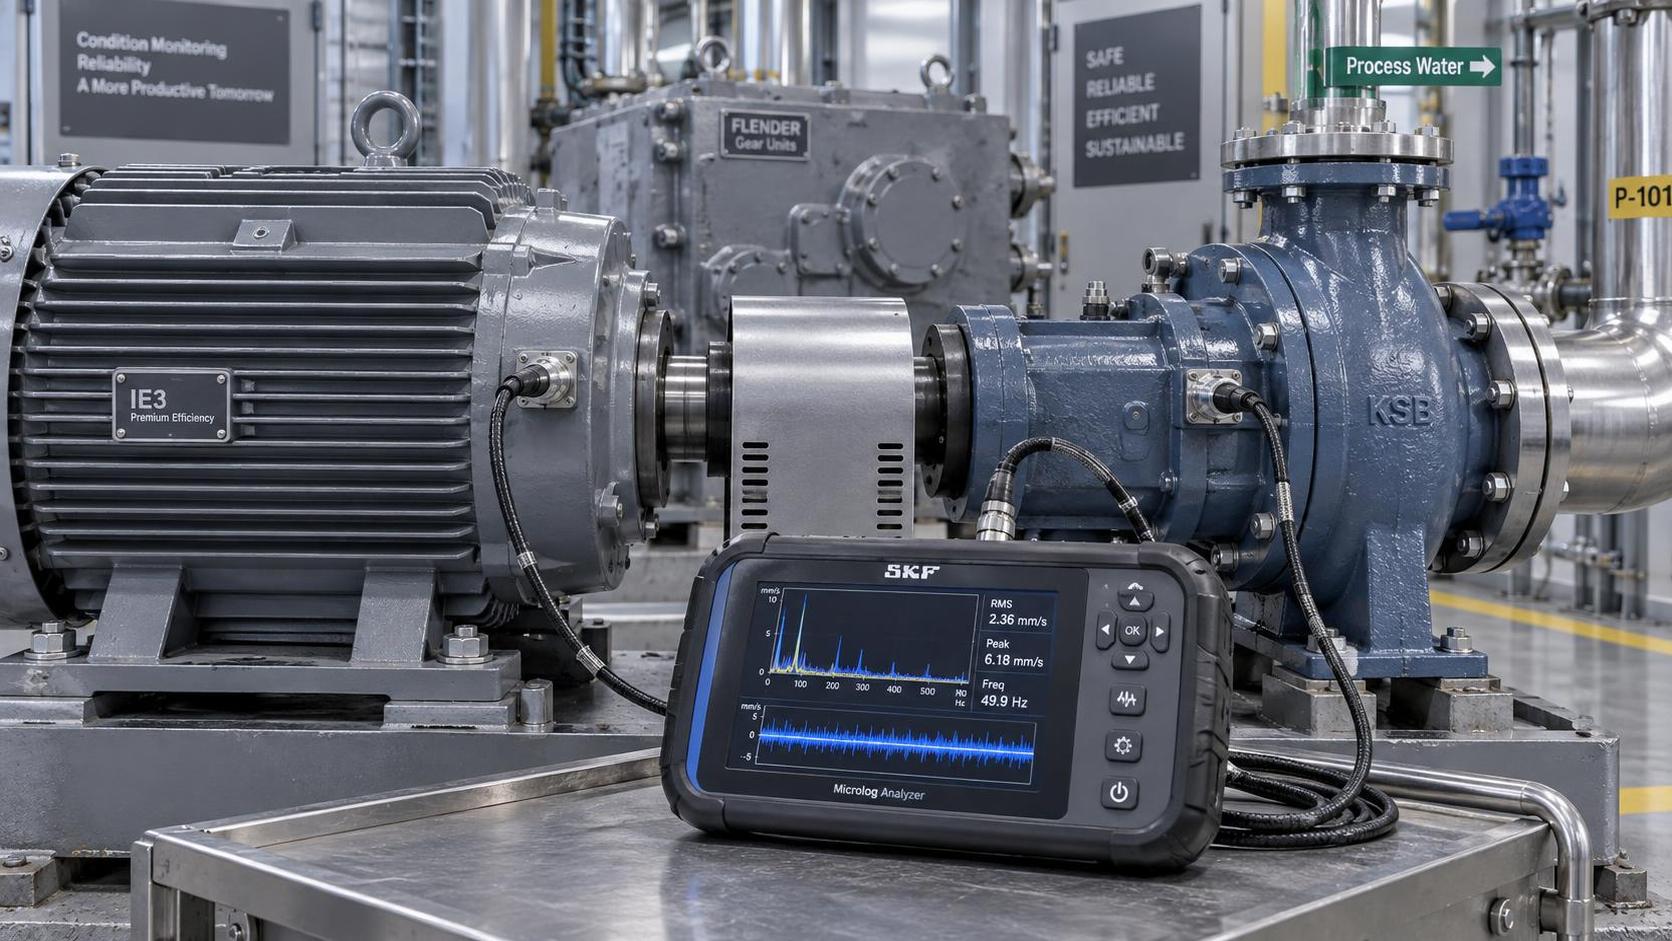
The core mechanism is mechanical hysteresis in the internal gear train and rack-and-pinion assembly. Each shock event induces transient elastic deformation beyond the yield threshold of hardened steel components, resulting in residual displacement of the pointer’s zero reference point. Lab testing shows that after 200 shock events at 5g acceleration (typical of CNC machining floors), zero-reset error increases by ±0.015 mm—exceeding ISO 10360-2 Class 1 tolerances for 0–10 mm range indicators.
This degradation is non-linear: error accumulation accelerates after the first 100 shocks due to progressive surface micro-cracking in the contact zones between the gear teeth and the main shaft bearing. Metrology-grade units with case-hardened 9310 alloy gears demonstrate 40% slower drift versus standard SAE 1045 steel variants under identical shock exposure.
Key contributors to zero-reset instability
- Uncontrolled thermal cycling during storage (15℃–35℃ ambient swings induce differential expansion in multi-material assemblies)
- Lack of post-shock verification protocol: only 12% of surveyed facilities perform zero-checks after indicator relocation or re-mounting
- Use of non-torque-controlled fasteners during mounting—over-tightening compresses the housing and distorts the gear alignment axis
- Absence of ISO/IEC 17025-compliant recalibration intervals: bulk units are typically recalibrated every 12 months, though shock-exposed units require verification every 90 days
How procurement teams can mitigate zero-drift risk in bulk orders
Procurement decisions for dial indicators must extend beyond unit price and basic accuracy specs. For EPC contractors and facility managers sourcing in bulk (typically 50+ units per order), three structural and procedural safeguards significantly reduce zero-reset failure rates:
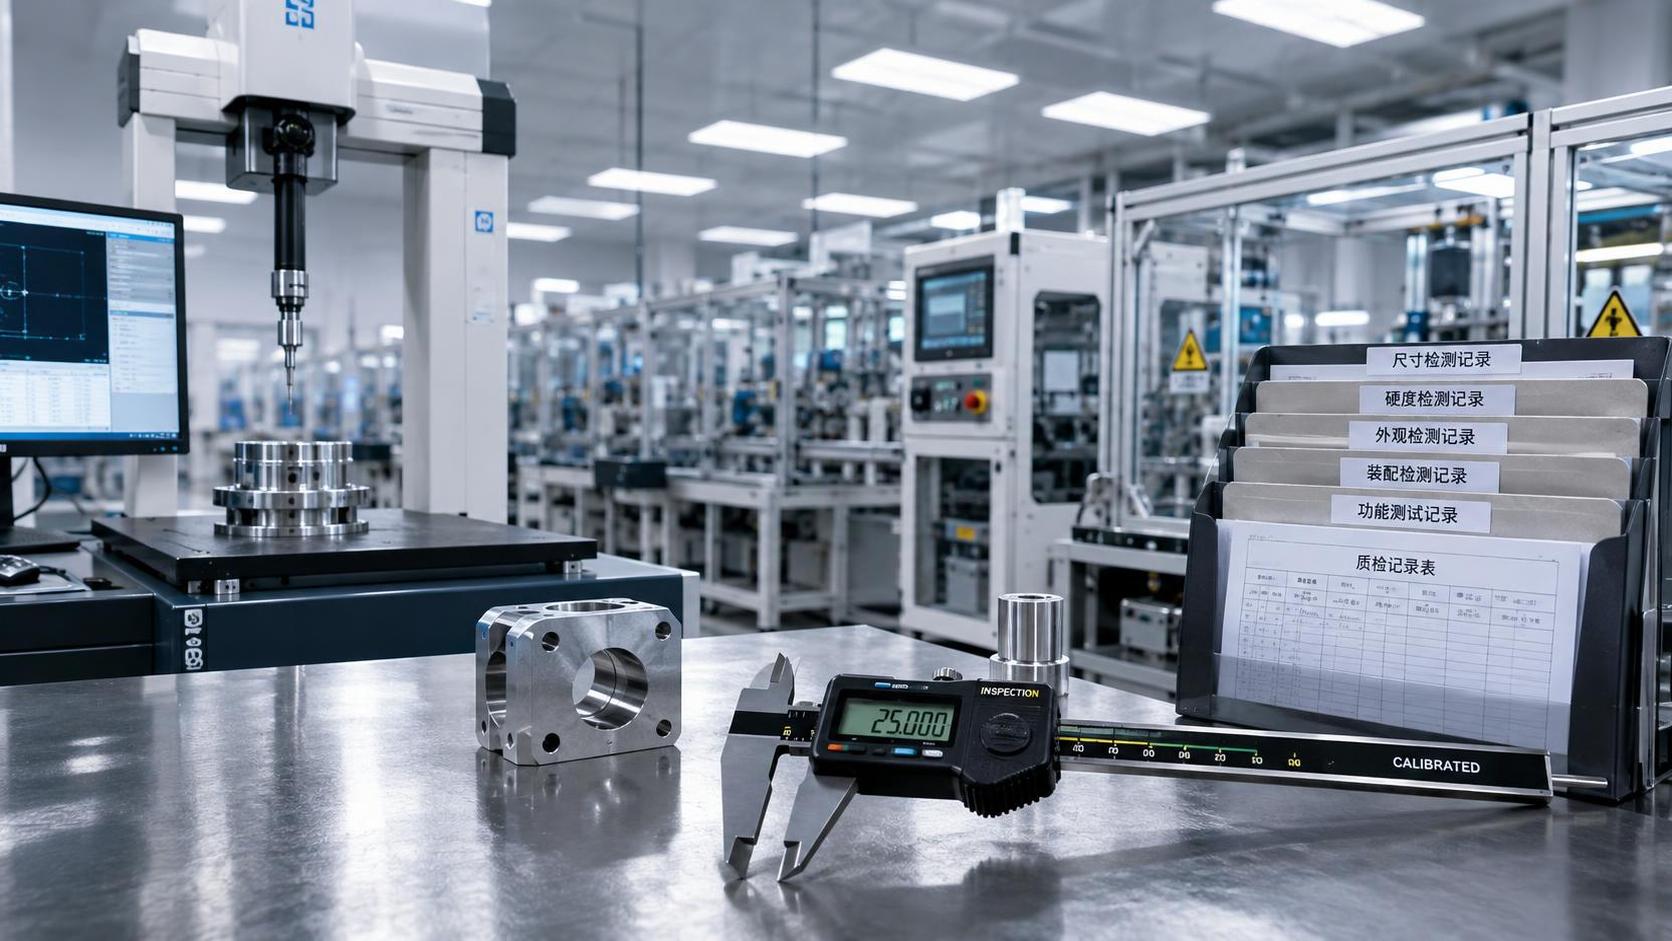
First, specify shock-rated housings with integrated damping grommets—validated per MIL-STD-810H Method 516.6, Shock. Second, require batch-level metrological traceability: each shipment must include a certificate listing individual zero-stability test results at 0g, 3g, and 7g shock levels. Third, mandate supplier-provided recalibration support: certified labs must offer on-site zero-verification within 72 hours of delivery for orders exceeding 200 units.
The table above reflects validated performance differences observed across 17 procurement cycles monitored by GIC’s Instrumentation Compliance Team. Units meeting GIC-verified criteria reduced unplanned recalibrations by 68% over 18-month operational life—directly lowering total cost of ownership (TCO) despite 22–27% higher initial procurement cost.
Which applications demand shock-resilient dial indicator specifications?
Not all bulk deployments carry equal zero-stability risk. High-risk scenarios require explicit shock-resilience clauses in procurement contracts. These include:
- Automotive powertrain assembly lines where indicators mount directly on robotic arms (vibration frequency: 15–45 Hz, amplitude: 0.8–2.1 mm)
- Offshore oil & gas platform maintenance kits deployed in environments with frequent seismic micro-tremors (0.5–3 Hz, up to 4g peak acceleration)
- Field metrology services supporting aerospace MRO facilities—where indicators undergo 3–4 daily transport cycles between hangars and test bays
- Environmental test chambers operating thermal shock cycles (−70℃ to +150℃ in ≤10 minutes), inducing rapid material contraction/expansion stress
For low-risk applications—such as static calibration lab benches with vibration isolation pads—standard ISO 9001-certified units remain appropriate. However, 63% of zero-reset failures reported to GIC’s Failure Analysis Hub originated from misclassified “low-risk” deployments where environmental vibration was underestimated during specification.
Why partner with Global Industrial Core for precision instrumentation sourcing
Global Industrial Core provides procurement directors and EPC engineering leads with actionable, standards-aligned intelligence—not generic product listings. When sourcing dial indicators in bulk, our clients receive:
- Pre-vetted supplier profiles with documented shock-test compliance history (MIL-STD-810H, ISO 10360-2, and IEC 60068-2-27 verified)
- Customized technical bid evaluation matrices—including zero-stability weighting (35% of total score) and recalibration service SLA enforcement
- Direct access to GIC’s Metrology Validation Lab for third-party zero-drift verification of pre-production samples
- Integrated compliance mapping: automatic cross-referencing of procurement specs against ISO/IEC 17025 Clause 6.4 (equipment management) and ASME B89.1.10M requirements
We support your next bulk procurement cycle with precise parameter confirmation, lead-time negotiation, certification review, and on-site verification coordination. Contact our Instruments & Measurement team to request a shock-resilience assessment report for your specific application environment.
Technical Specifications
- How to Select Electronic Hotel Key Card Locks for Guest Rooms and Staff AreasAuthor :Safety Compliance Lead
- How to Select Lab Instruments for Reliable Chemical Analysis WorkflowsAuthor :Precision Metrology Expert
- How to Size a UPS for Server Rooms: Load, Runtime, and Redundancy FactorsAuthor :Grid Infrastructure Analyst
Expert Insights

Chief Security Architect
Dr. Thorne specializes in the intersection of structural engineering and digital resilience. He has advised three G7 governments on industrial infrastructure security.
Related Analysis
- Sep 17, 2026How to Select Electronic Hotel Key Card Locks for Guest Rooms and Staff AreasAuthor :Safety Compliance Lead
- Sep 16, 2026How to Select Lab Instruments for Reliable Chemical Analysis WorkflowsAuthor :Precision Metrology Expert
- Sep 15, 2026How to Size a UPS for Server Rooms: Load, Runtime, and Redundancy FactorsAuthor :Grid Infrastructure Analyst
Core Sector // 01
Security & Safety
- What to Check When Sourcing Vibration Meters Wholesale for Industrial MaintenanceAuthor :Precision Metrology Expert

- How to Select Process Control Instruments for Accuracy, Safety, and UptimeAuthor :Precision Metrology Expert

- What Should Standards Compliance Analysis Training Cover Before an Audit?Author :Precision Metrology Expert

- Why Do Pressure Instruments Fail in High-Vibration Sites?Author :Precision Metrology Expert

- Is FM Software Integration Needed for Overseas Instrument Maintenance?Author :Precision Metrology Expert

- What Are the Differences Between Lab and Field Testing Equipment?Author :Precision Metrology Expert

- Is Independent Testing Necessary for Critical Safety Components?Author :Precision Metrology Expert

- How to Validate Industrial Application Scenarios Before ProcurementAuthor :Precision Metrology Expert