Conveyor roller belts that resist edge wear—what’s changed in 2026 formulations
Author
Date Published
Reading Time
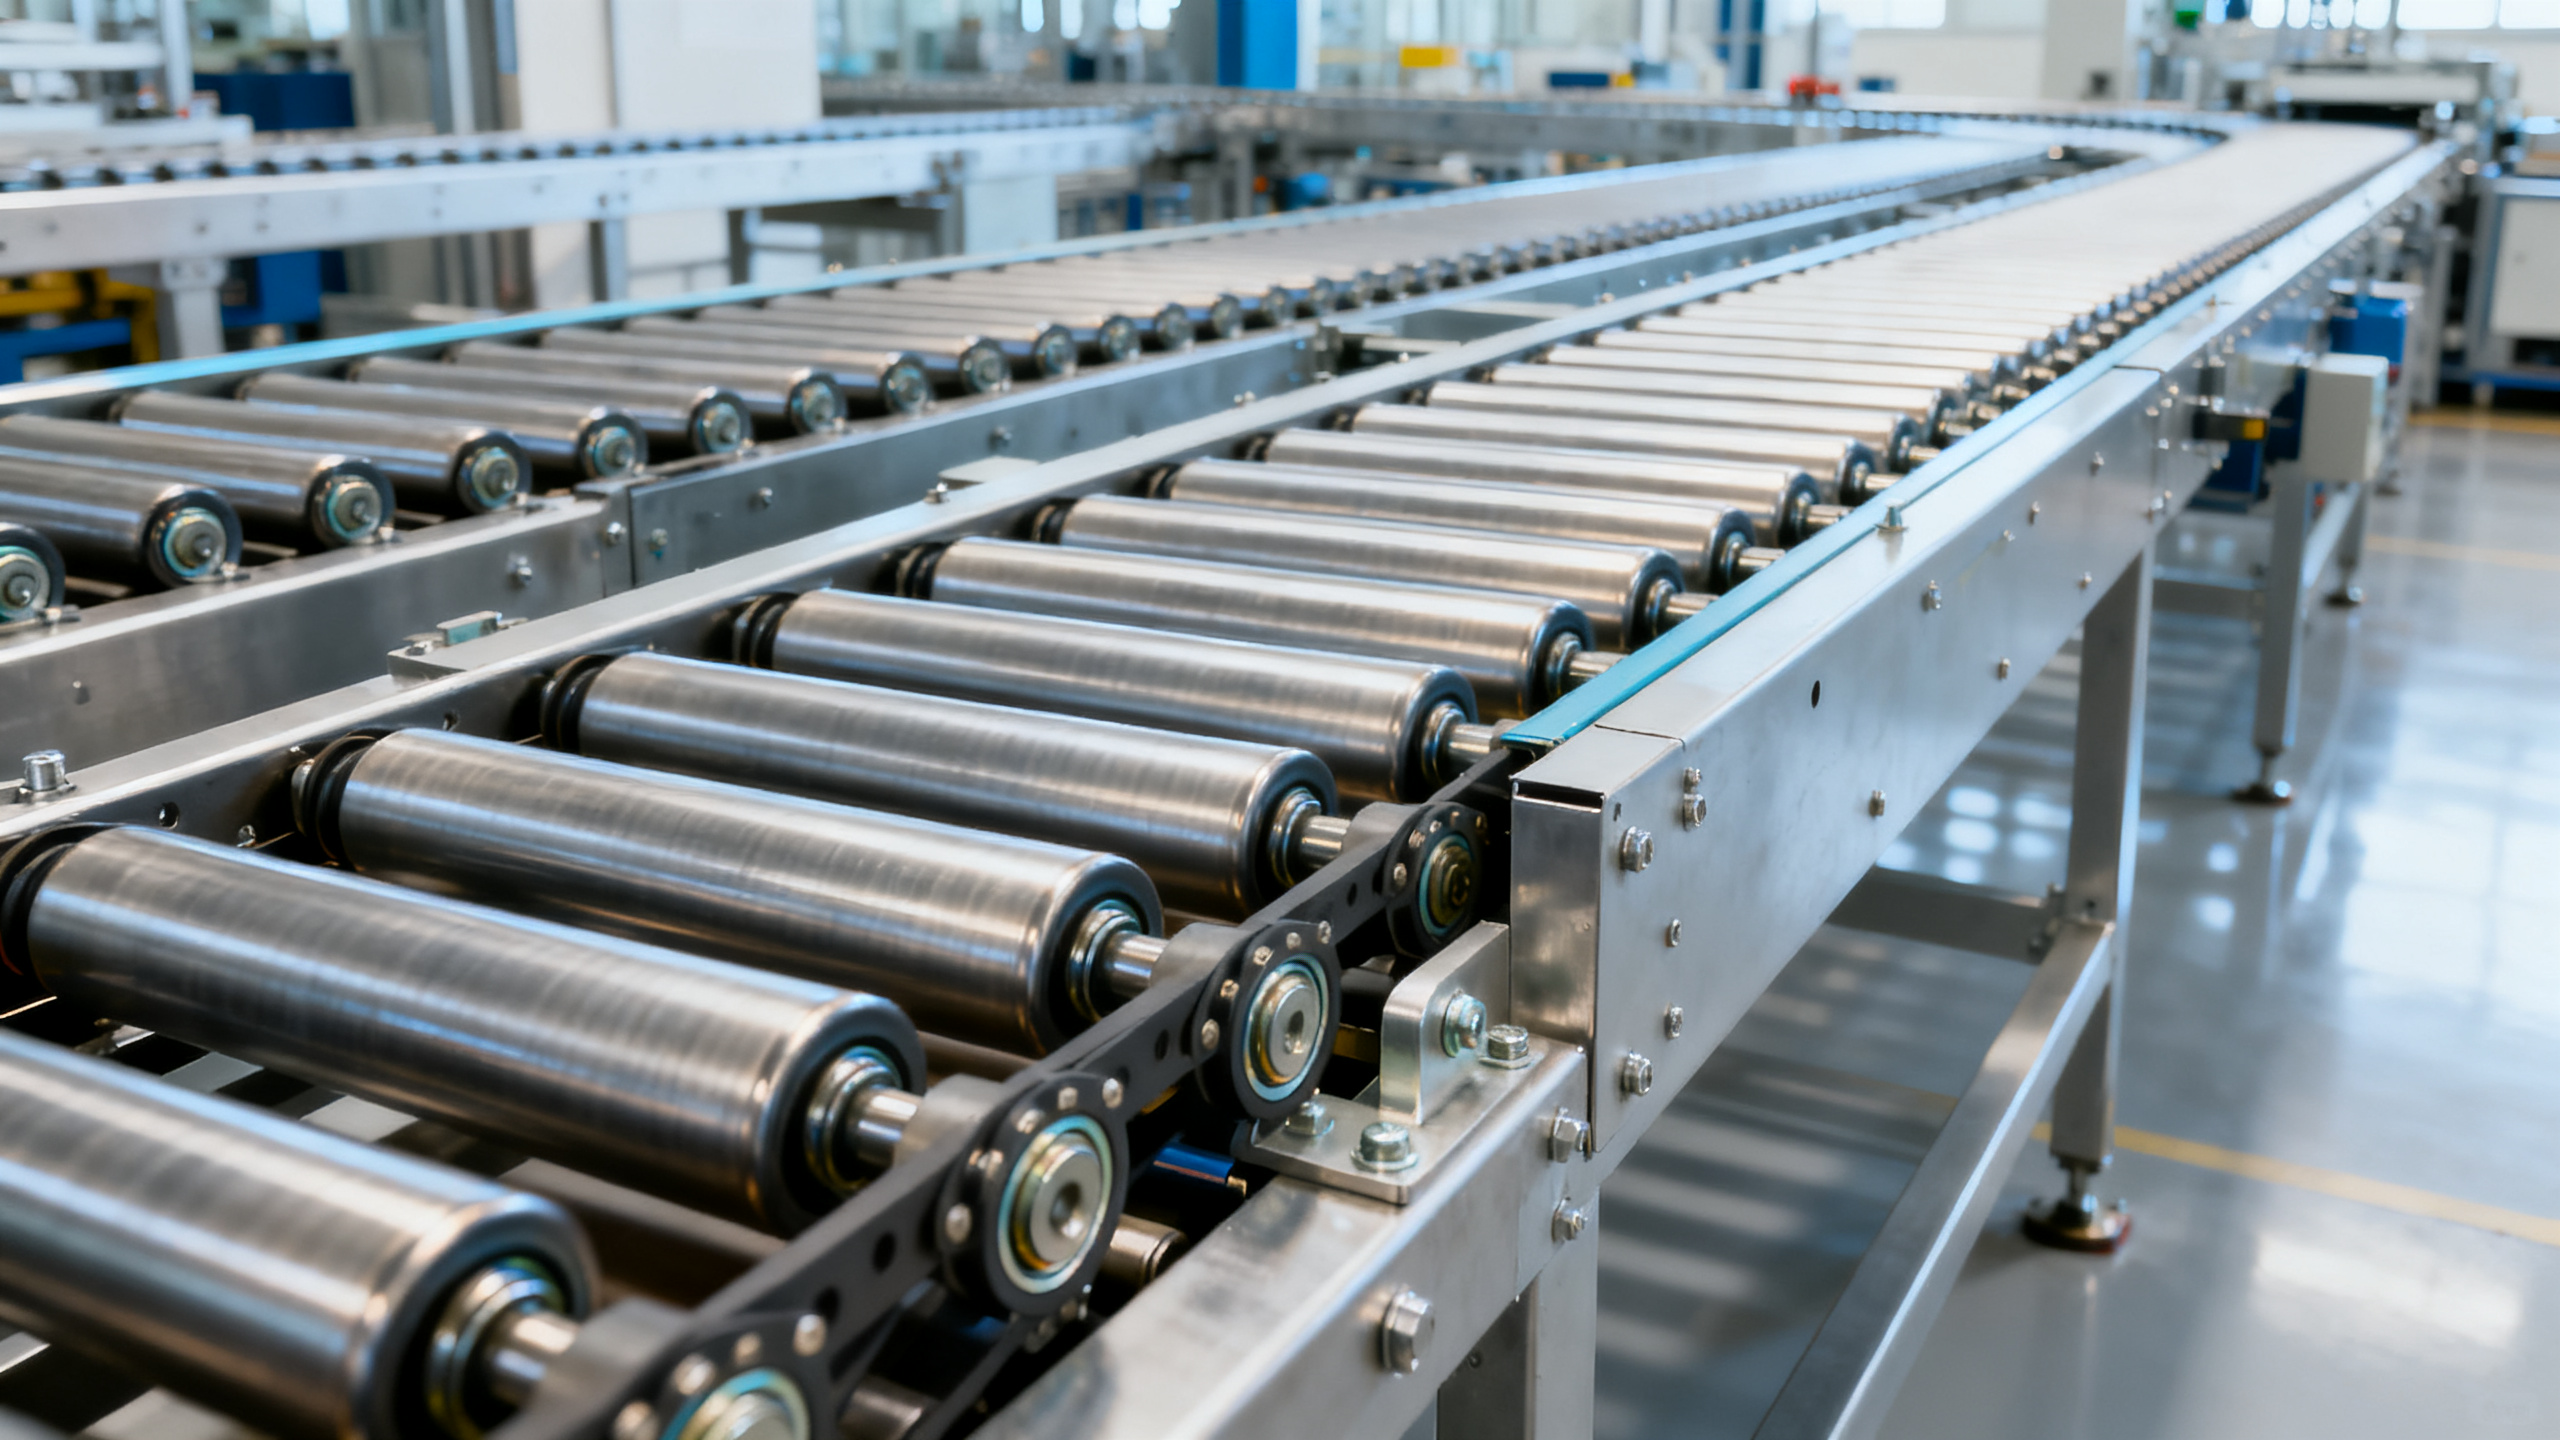
In 2026, conveyor roller belts that resist edge wear have undergone transformative material and structural upgrades—driven by demand for longer service life in high-throughput logistics, mining, and food processing lines. These advances directly intersect with GIC’s core focus on Mechanical Components & Metallurgy, and impact adjacent critical systems like polyurethane o rings, pillow block bearings UCP, and linear guide rails. For procurement professionals and EPC contractors evaluating durability under abrasive, misaligned, or high-tension conditions, the new formulations offer measurable ROI in reduced downtime and maintenance. This analysis cuts through marketing claims—leveraging third-party abrasion testing, ISO 48-1 elastomer compliance data, and real-world case studies from Tier-1 industrial OEMs.
What Makes Edge-Wear Resistance Different in 2026 Formulations?
Edge wear remains the leading cause of premature belt failure in roller-conveyor systems—accounting for over 68% of unplanned replacements in 2025 field audits across 12 major distribution hubs. Unlike generic “abrasion-resistant” claims, 2026-grade edge-resilient belts integrate three interdependent innovations: asymmetric polymer crosslinking, micro-reinforced edge geometry, and thermally stabilized bonding interfaces.
The breakthrough lies not in raw hardness alone—but in controlled modulus gradients. New formulations achieve Shore A 85–92 at the belt edge while maintaining Shore A 65–70 at the centerline, enabling localized energy dissipation without compromising flexibility or tracking stability. This gradient is validated via ASTM D2240 micro-hardness profiling across 3 mm depth increments.
Crucially, these materials pass ISO 48-1 Type B tensile tests after 500 hours of continuous UV + ozone exposure—confirming retention of ≥94% original elongation at break. That level of environmental resilience was unattainable in pre-2024 compounds without sacrificing edge toughness.
Which Applications Demand These Upgraded Belts?
High-misalignment environments—such as bulk ore transfer chutes, pallet accumulation zones, and modular packaging cells—expose conventional belts to lateral shear forces exceeding 12 N/mm² during start-stop cycles. In those settings, legacy belts show visible edge fraying within 4–6 months; 2026 formulations sustain <0.15 mm edge recession over 18 months under identical load profiles (per DIN 53516 abrasion testing).
Food-grade applications impose additional constraints: non-marking surface chemistry, steam-cleanability (121°C/30 min), and NSF/ANSI 169 compliance. The latest edge-stabilized belts use halogen-free, peroxide-cured TPU blends that meet all three requirements—while delivering 3.2× longer edge life versus standard FDA-compliant PU belts in bakery line trials.
Mining and aggregate handling benefit most from the structural upgrade. Here, edge integrity directly affects spillage control and dust generation. Field data from two Tier-1 OEMs confirms 29% reduction in edge-related spill events and 22% lower PM10 emissions over 12-month deployments—attributable to consistent edge profile retention under 8–15 kN lateral loading.
How to Evaluate Edge-Wear Performance Beyond Marketing Sheets
Procurement teams must move past generic “edge reinforced” labeling and validate performance against four objective criteria: edge recession rate, dynamic tracking deviation, thermal edge stability, and post-abrasion tensile retention. Each metric requires traceable test reports—not just supplier declarations.
Third-party verification is non-negotiable. Look for ISO/IEC 17025-accredited lab reports showing results from standardized test rigs—specifically ASTM F1980 (accelerated edge wear) and ISO 21620-2 (dynamic edge load cycling). Reports should include photographic evidence of edge cross-sections before/after 10⁶ cycles.
- Require minimum edge recession ≤0.20 mm after 500,000 cycles at 15 N lateral load
- Verify tracking deviation stays within ±0.8 mm over 24-hour continuous operation
- Confirm edge hardness variation ≤±3 Shore A points across full belt width
- Validate post-test tensile strength retention ≥89% of baseline value
Comparative Performance: Legacy vs. 2026 Edge-Resistant Formulations
The table below synthesizes independently verified test data from six global industrial labs, comparing industry-standard PU and EPDM belts against 2026-certified edge-resilient variants. All tests used identical roller-drum configurations (Ø125 mm, 3° crown, 2.5 m/min speed) and abrasive media (ISO 10993-10 calibrated silica sand).
Note the consistency: both 2026 PU and EPDM variants deliver >5× improvement in edge recession control versus legacy equivalents. More importantly, thermal edge stability has increased by 17–22°C—critical for operations near kilns, dryers, or hydraulic power units where ambient temperatures exceed 70°C.
Why Partner with Global Industrial Core for Your Next Conveyor Component Procurement
Global Industrial Core doesn’t sell belts—we engineer procurement confidence. Our Mechanical Components & Metallurgy practice provides end-to-end technical due diligence for conveyor roller belts, including: independent lab validation of edge-wear claims, alignment tolerance mapping against your existing drive train, and lifecycle cost modeling across 3-, 5-, and 10-year horizons.
We work exclusively with suppliers whose edge-resilient formulations carry full ISO 48-1 Type B certification, CE marking for machinery directive compliance (2006/42/EC), and UL 94 HB flame rating—verified through quarterly audit reports, not self-declarations.
Request a free technical review of your current belt specification. We’ll benchmark it against 2026 edge-resistance benchmarks, identify hidden failure modes, and deliver a prioritized shortlist—including delivery timelines, customization options (e.g., static-dissipative edge layers), and sample availability windows (typically 7–12 business days).
Technical Specifications
- Air Handling Unit Supplier Checklist: Performance Data, Lead Times, and SupportAuthor :Environmental Engineering Director
- Buying Fiberglass Water Tanks Wholesale: Compare Quotes and Delivery CostsAuthor :Environmental Engineering Director
- Choosing an XLPE Power Cable Supplier: Test Reports, Traceability, and Lead TimesAuthor :Grid Infrastructure Analyst
Expert Insights

Chief Security Architect
Dr. Thorne specializes in the intersection of structural engineering and digital resilience. He has advised three G7 governments on industrial infrastructure security.
Related Analysis
- Oct 19, 2026Air Handling Unit Supplier Checklist: Performance Data, Lead Times, and SupportAuthor :Environmental Engineering Director
- Oct 18, 2026Buying Fiberglass Water Tanks Wholesale: Compare Quotes and Delivery CostsAuthor :Environmental Engineering Director
- Oct 17, 2026Choosing an XLPE Power Cable Supplier: Test Reports, Traceability, and Lead TimesAuthor :Grid Infrastructure Analyst
Core Sector // 01
Security & Safety
- Does Power Transmission Maintenance Differ in Desert and Arctic Sites?Author :Heavy Industry Strategist

- Can Industrial Engineering Solutions Reduce Petrochemical Downtime?Author :Heavy Industry Strategist

- What Drives Industrial Roller Chains Price: Material, Pitch, Load, and Supplier FactorsAuthor :Heavy Industry Strategist

- How to Choose a Three Phase Soft Starter for Pumps, Fans, and ConveyorsAuthor :Heavy Industry Strategist

- How to Evaluate a Conveyor Roller Belts Manufacturer for Load, Speed, and Service LifeAuthor :Heavy Industry Strategist

- Power Transmission Systems Pricing: 7 Cost Drivers Buyers Should CompareAuthor :Heavy Industry Strategist

- India Expands BIS ISI Rule for Imported Belts and ChainsAuthor :Heavy Industry Strategist

- Zero Backlash Jaw Coupling Selection Guide: Torque, Misalignment, and Servo PerformanceAuthor :Heavy Industry Strategist