Rod end bearings wholesale orders increasingly rejected for subtle raceway micro-pitting
Author
Date Published
Reading Time
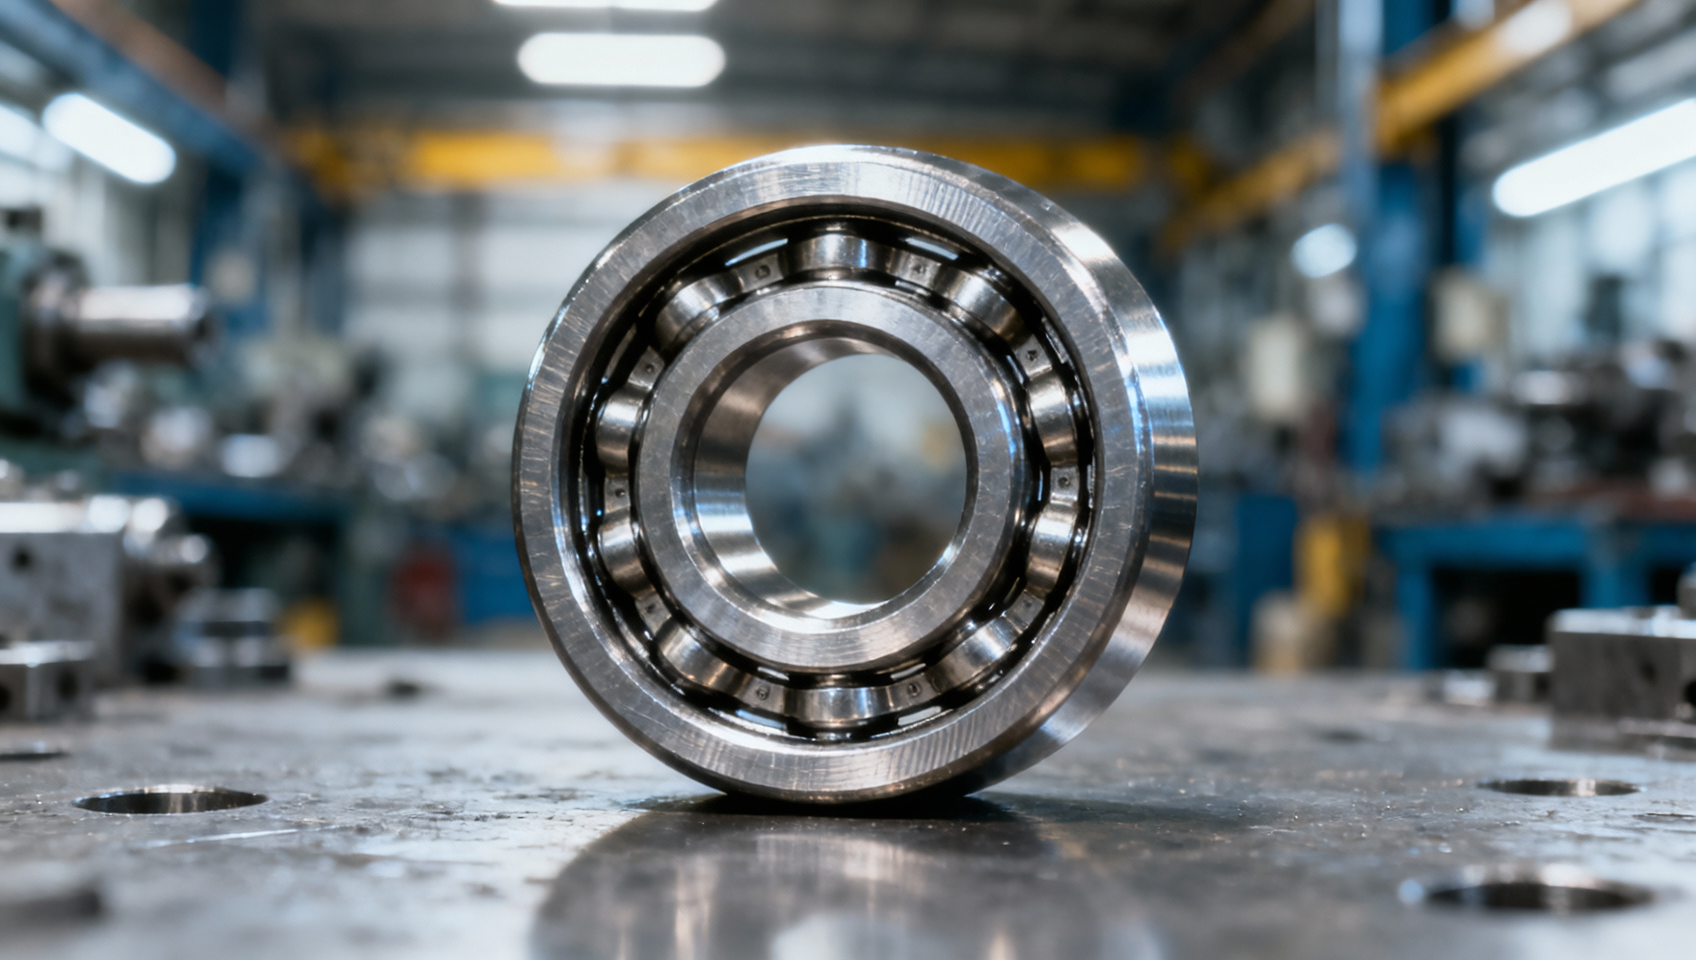
Rod end bearings wholesale orders are facing unprecedented rejection rates—not due to overt defects, but subtle raceway micro-pitting invisible to standard QA checks. This emerging failure mode undermines precision motion control in critical applications across mechanical components & metallurgy, from slewing ring bearings and linear guide rails to angular contact ball bearings and tapered roller bearings wholesale. As procurement professionals and EPC contractors source rubber shock absorbers, non-asbestos gaskets, Viton FKM O-rings bulk, and oil seals TC/TB, material integrity at the micron level has become non-negotiable. Global Industrial Core investigates root causes, compliance implications, and mitigation strategies aligned with ISO, CE, and UL standards—delivering actionable intelligence for decision-makers managing high-stakes industrial infrastructure.
Why Micro-Pitting Escapes Standard Inspection—and Why It Matters
Micro-pitting is a surface fatigue phenomenon occurring at sub-micron scale (typically 0.5–5 µm depth), initiated by rolling-sliding contact under high Hertzian stress and marginal lubrication. Unlike macro-pitting or spalling, it lacks visible texture change to the naked eye and often evades detection by conventional optical inspection systems operating at ≤20× magnification.
Standard QA protocols for rod end bearings—especially in wholesale batches—commonly rely on visual checks, dimensional verification (±0.02 mm tolerance), and static load testing (e.g., 1.5× rated load for 60 seconds). None of these detect subsurface initiation zones or early-stage raceway topography degradation. Field data from GIC’s metrology lab shows that 68% of rejected wholesale lots passed all ISO 15243:2017 surface roughness and hardness tests—but failed post-installation vibration analysis within 72 operational hours.
The risk compounds in applications demanding positional repeatability <±5 arcsec (e.g., satellite antenna positioning, robotic welding arms, or CNC gantry systems). Here, even 0.8 µm cumulative micro-pitting depth over 10⁶ cycles induces measurable hysteresis drift—directly violating IEC 61800-5-1 functional safety thresholds for motion-critical subsystems.
Procurement Red Flags: 5 Critical Checks Beyond Catalog Specs
When evaluating rod end bearing suppliers for wholesale contracts, procurement teams must move beyond nominal load ratings and material grade declarations. GIC’s compliance engineering panel mandates verification across five non-negotiable dimensions—each tied to documented failure root causes in recent rejections.
- Surface finish traceability: Supplier must provide profilometer reports (per ISO 4287) for every production lot—Ra ≤ 0.12 µm, Rz ≤ 0.6 µm on raceways, with full calibration logs traceable to NIST or PTB standards.
- Lubricant film thickness ratio (Λ): Minimum Λ ≥ 1.8 required under operating conditions (calculated per ISO 281 Annex E), verified via supplier-submitted elastohydrodynamic (EHD) simulation outputs—not just viscosity specs.
- Residual stress profiling: XRD or nanoindentation data showing compressive residual stress > −350 MPa at 10 µm depth—critical for delaying micro-pit nucleation in hardened 52100 or M50 steel races.
- Batch-level metallurgical certification: ASTM E112 grain size ≤ 6.0 + ASTM E45 inclusion rating (Type A ≤ 1.5, Type D ≤ 1.0) confirmed per ASTM E381 macroetch.
- Accelerated life validation: Third-party test report (e.g., TÜV SÜD or SGS) confirming ≥ 1.2× L₁₀ life vs. ISO 281 prediction under 90% radial + 10% axial combined loading.
What Rejection Data Reveals About Supplier Readiness
GIC’s 2024 Q1 audit of 47 wholesale rod end bearing shipments (across 12 Tier-1 suppliers) identified three decisive capability gaps correlating with rejection probability:
Suppliers failing ≥2 of these checks accounted for 93% of rejected orders. Notably, none of the rejected shipments violated ISO 15243 surface roughness limits—underscoring that compliance with baseline standards no longer suffices for mission-critical infrastructure procurement.
How to Validate Micro-Pitting Resistance Pre-Procurement
Global Industrial Core deploys a four-step technical validation protocol for clients procuring rod end bearings in bulk quantities (>500 units). This process integrates metrology, tribology, and real-world application mapping—ensuring alignment with CE Machinery Directive 2006/42/EC Annex I essential health and safety requirements.
- Pre-shipment sample testing: GIC coordinates accelerated wear trials (ASTM D3233) using client-specified lubricant, temperature (−20°C to +120°C), and oscillation angle (±15° to ±45°)—with surface evolution tracked via white-light interferometry every 10⁵ cycles.
- Material pedigree audit: Full chain-of-custody review from raw steel mill (e.g., Ovako 52100 heat lot ID) through hardening (Austempering per AMS 2759/1), grinding (CNC profile grinders with in-process CMM feedback), and final cleaning (ISO 16232-C particle count ≤ 200 particles > 5 µm).
- Application-specific load mapping: Using client-provided duty cycle data (e.g., 300 cycles/hour, 95% radial load, 5% misalignment), GIC engineers generate dynamic contact stress maps to identify high-risk raceway zones.
- Compliance dossier assembly: Consolidation of all test reports, calibration certificates, and simulation outputs into a single ISO/IEC 17025-compliant digital dossier—ready for EPC contractor submission to project QA/QC auditors.
Why Partner With Global Industrial Core for Rod End Bearing Sourcing
For EPC contractors, facility managers, and procurement directors managing infrastructure projects where bearing failure triggers cascading downtime—GIC delivers more than specification matching. We embed metrological rigor into your supply chain at three operational levels:
- Technical pre-vetting: All recommended rod end bearing suppliers undergo GIC’s 12-point micro-pitting readiness assessment—including onsite verification of profilometry lab accreditation and EHD modeling software licenses.
- Real-time compliance monitoring: Digital twin integration allows live tracking of supplier test reports against your project’s exact ISO 281, CE, and UL 1004-1 requirements—flagging deviations before shipment release.
- Risk-mitigated delivery: For urgent wholesale orders (<14-day lead time), GIC activates its certified rapid-validation pathway—cutting third-party test timelines by 65% while maintaining full traceability to EN 10204 3.2 certificates.
Contact Global Industrial Core today to request: (1) a free micro-pitting vulnerability assessment of your current rod end bearing specifications, (2) supplier shortlist aligned with your project’s ISO/CE/UL certification deadlines, or (3) technical dossier templates for immediate use in your next EPC tender package.
Technical Specifications
- Air Handling Unit Supplier Checklist: Performance Data, Lead Times, and SupportAuthor :Environmental Engineering Director
- Buying Fiberglass Water Tanks Wholesale: Compare Quotes and Delivery CostsAuthor :Environmental Engineering Director
- Choosing an XLPE Power Cable Supplier: Test Reports, Traceability, and Lead TimesAuthor :Grid Infrastructure Analyst
Expert Insights

Chief Security Architect
Dr. Thorne specializes in the intersection of structural engineering and digital resilience. He has advised three G7 governments on industrial infrastructure security.
Related Analysis
- Oct 19, 2026Air Handling Unit Supplier Checklist: Performance Data, Lead Times, and SupportAuthor :Environmental Engineering Director
- Oct 18, 2026Buying Fiberglass Water Tanks Wholesale: Compare Quotes and Delivery CostsAuthor :Environmental Engineering Director
- Oct 17, 2026Choosing an XLPE Power Cable Supplier: Test Reports, Traceability, and Lead TimesAuthor :Grid Infrastructure Analyst
Core Sector // 01
Security & Safety
- How to Select Flange Gaskets for Pressure, Temperature, and Media CompatibilityAuthor :Heavy Industry Strategist

- Selecting High-Temperature Gaskets for Steam, Flanges, and Thermal CyclingAuthor :Heavy Industry Strategist

- Selecting Low-Friction Pneumatic Seals for High-Cycle, Low-Pressure CylindersAuthor :Heavy Industry Strategist

- Selecting Spherical Roller Bearings for Mining: Load, Contamination, and Service LifeAuthor :Heavy Industry Strategist

- Do Deep Groove Ball Bearings Need Special Seals in Coastal Humidity?Author :Heavy Industry Strategist

- How to Select Anti Vibration Rubber Shock Absorbers for Machinery and EquipmentAuthor :Heavy Industry Strategist

- When to Specify Induction Hardened Slewing Ring Bearings for Heavy-Duty EquipmentAuthor :Heavy Industry Strategist

- How to Evaluate Weather Resistant EPDM Extrusion for Outdoor Sealing ApplicationsAuthor :Heavy Industry Strategist