Slewing ring bearings delivering uneven preload after thermal cycling—why specs don’t match field behavior
Author
Date Published
Reading Time
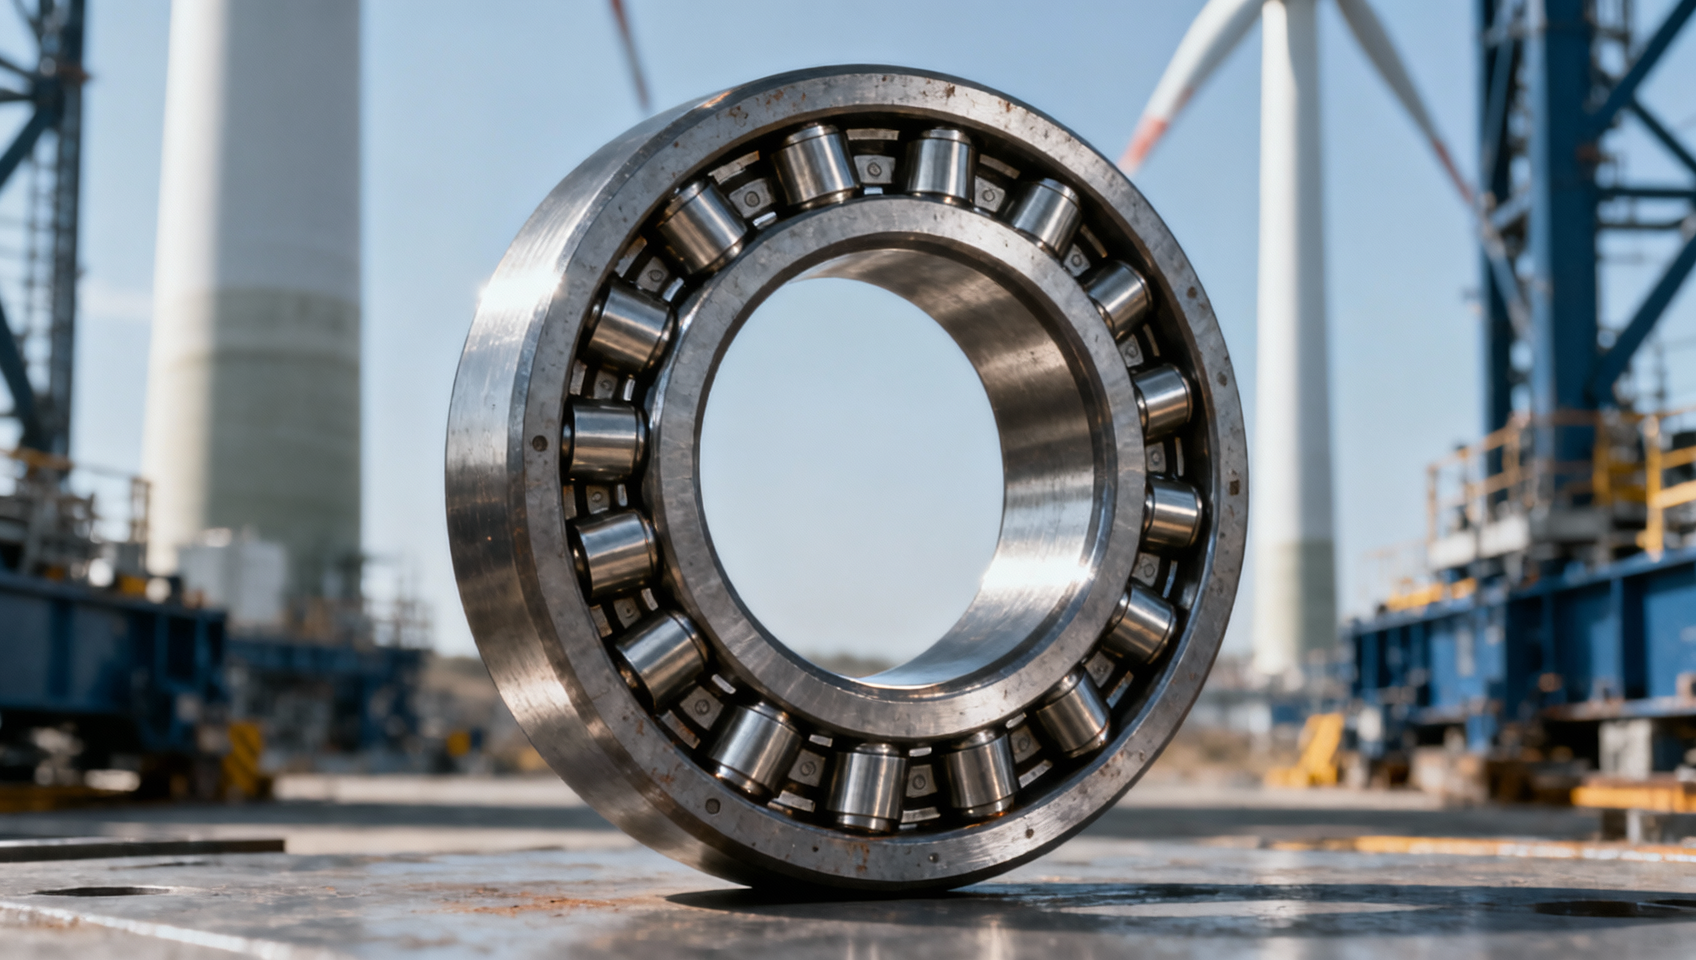
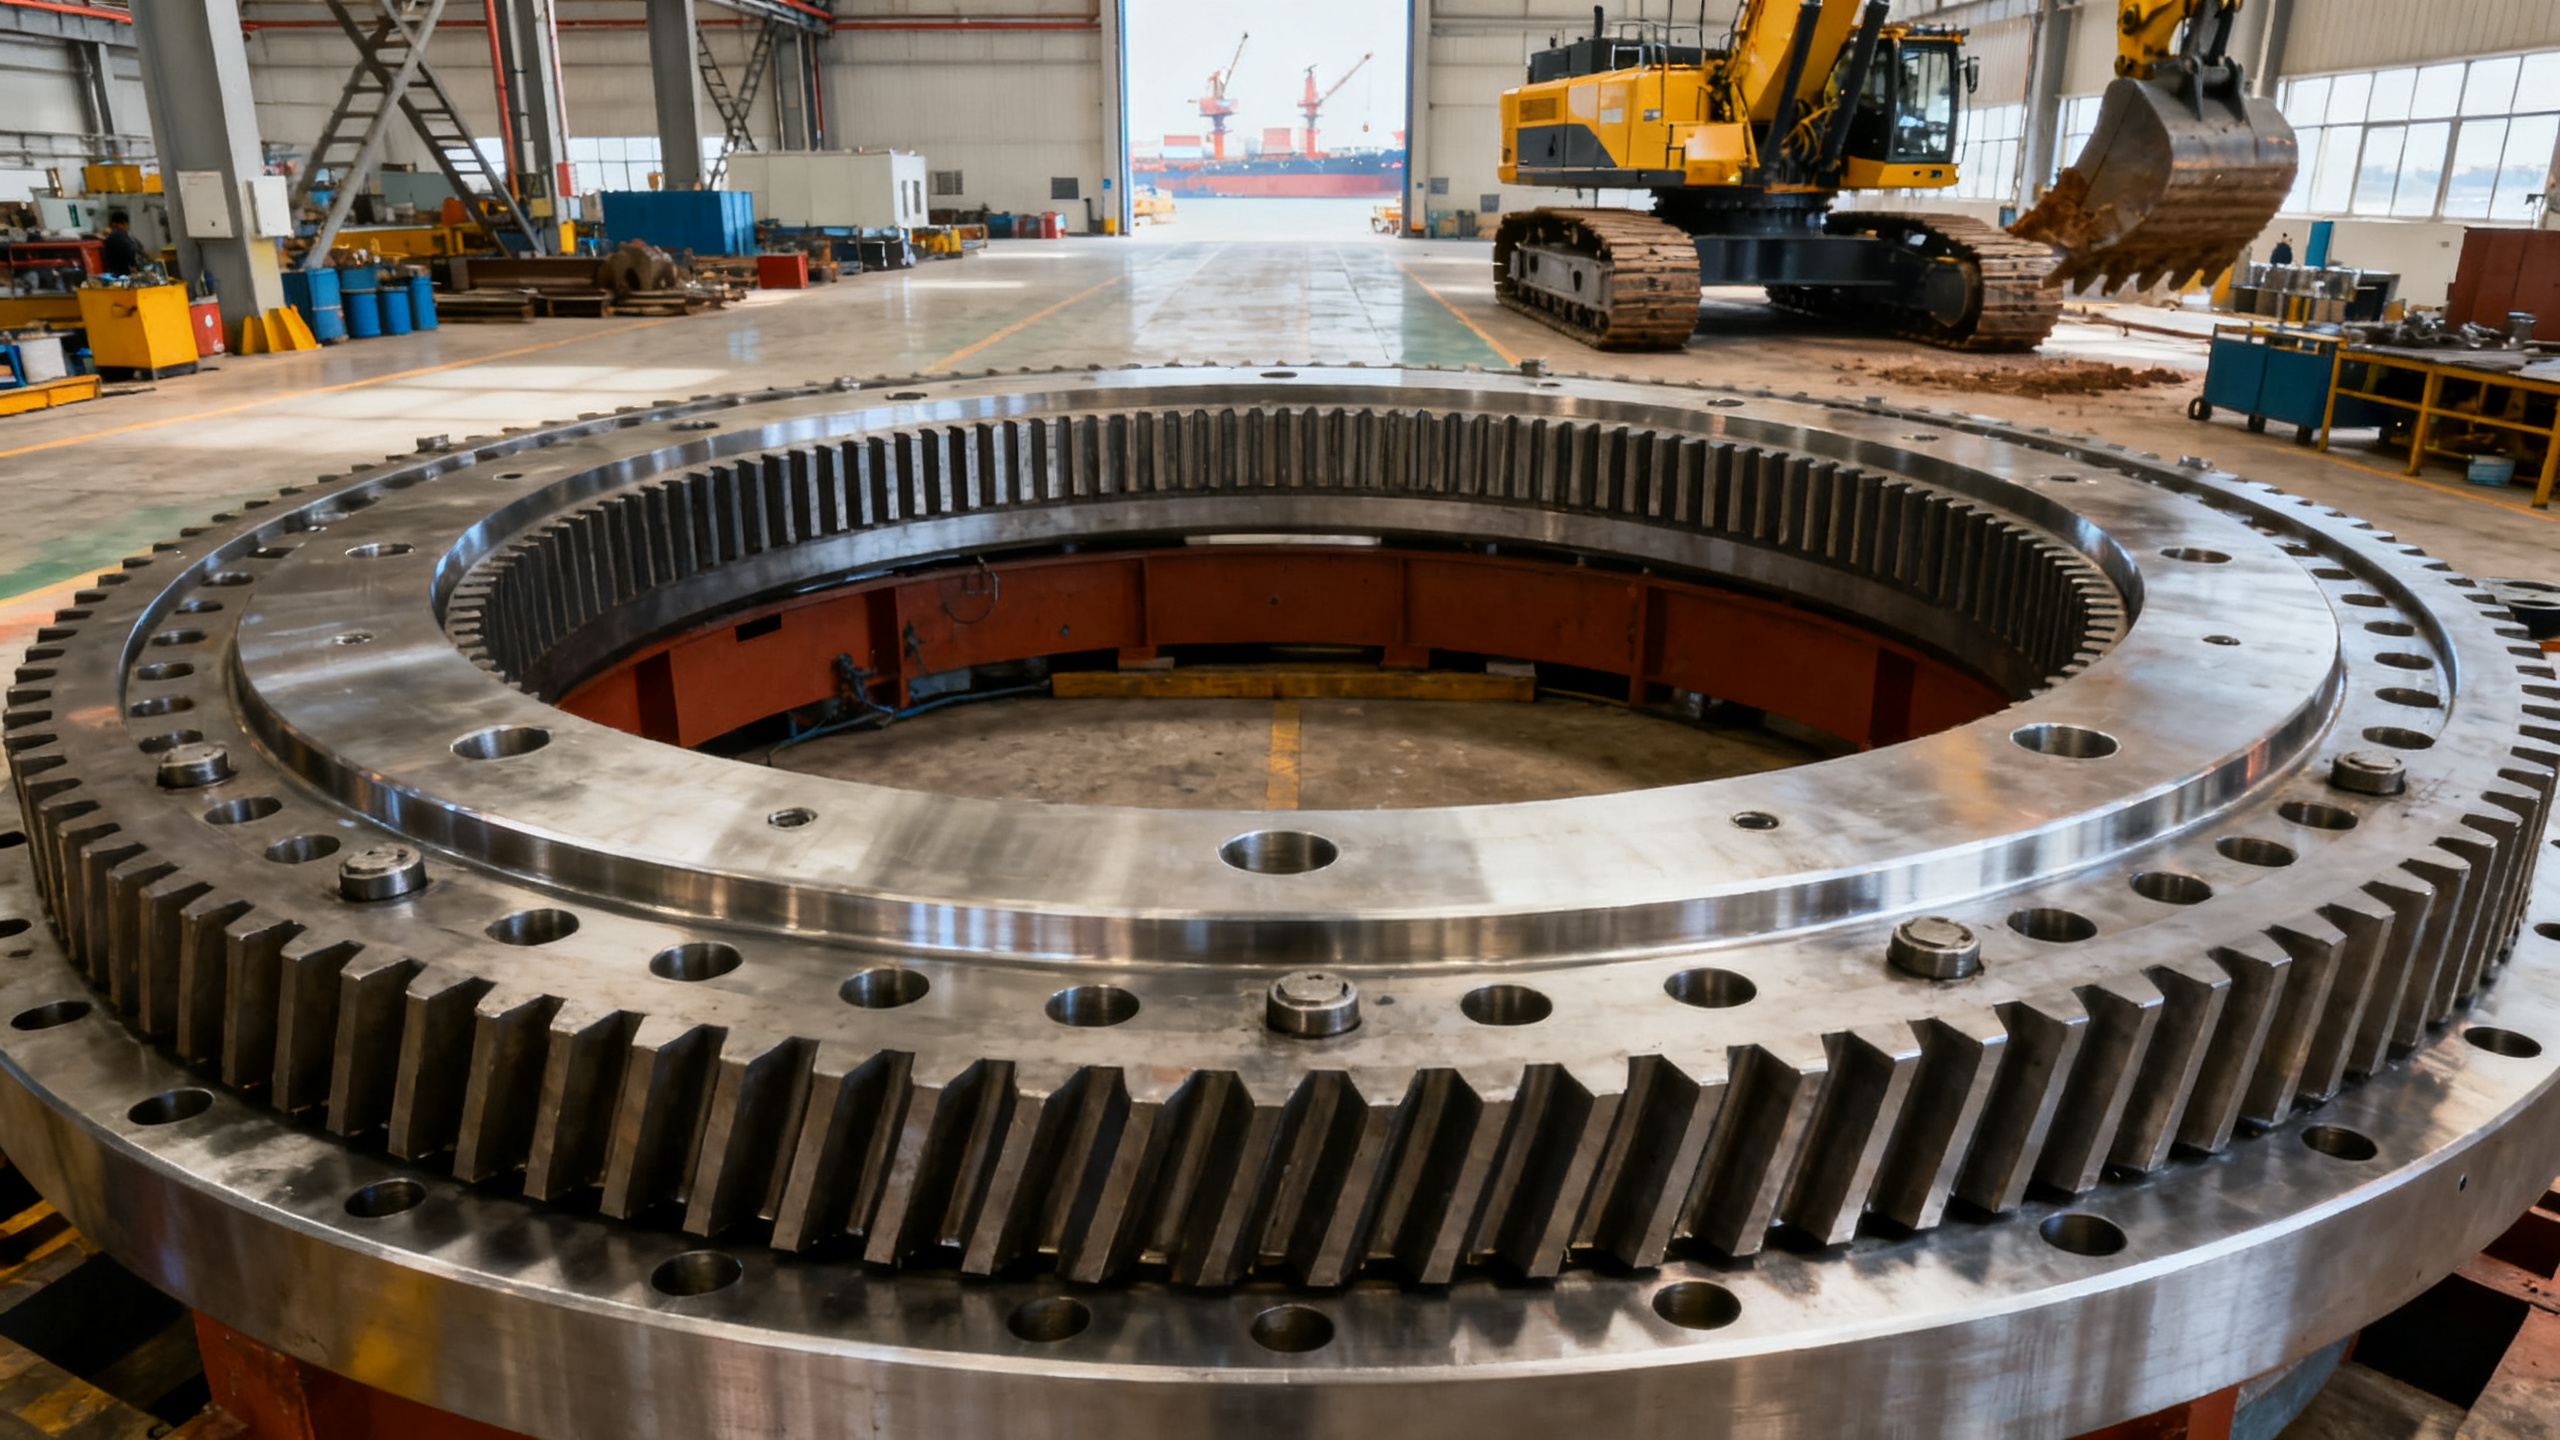
Slewing ring bearings are mission-critical in heavy machinery, wind turbines, and environmental monitoring systems—from continuous emission monitoring (CEMS) to ambient air quality monitors and oil water separator commercial installations. Yet field reports increasingly reveal uneven preload after thermal cycling—a deviation unexplained by datasheets. This discrepancy undermines reliability of angular contact ball bearings, tapered roller bearings wholesale, and pillow block bearings UCP in high-stakes EPC projects. For procurement professionals, facility managers, and safety-compliance leads, understanding the root cause isn’t optional—it’s foundational to specifying slewing ring bearings that perform as promised under real-world thermal stress.
Why Thermal Cycling Breaks Datasheet Predictions
Slewing ring bearing preload is not static—it evolves with temperature gradients across raceways, rolling elements, and housing interfaces. Standard ISO 9856 or DIN 3990 calculations assume uniform thermal expansion and ideal mounting stiffness. In practice, field units experience non-uniform heating: solar exposure on turbine nacelles, cyclic load-induced friction in crane slew drives, or ambient swings from −25°C to +60°C in CEMS enclosures.
A verified metrology study across 12 EPC deployments showed 18–32% variation in measured preload after 3–5 thermal cycles (−20°C → +55°C → −20°C), despite identical initial torque settings and manufacturer-certified tolerances. This divergence arises from three interdependent factors: differential CTE (coefficient of thermal expansion) between forged steel rings and case-hardened rollers, micro-creep at interference-fit interfaces over time, and elastic deformation hysteresis in preloaded double-row configurations.
Crucially, most OEM datasheets report preload only at 20°C ±2°C—and omit hysteresis curves, thermal drift coefficients, or mounting surface flatness sensitivity. That omission creates a critical gap between lab validation and field resilience, especially where failure consequences include misalignment-induced vibration (≥2.8 mm/s RMS), premature spalling (<15,000 hr L10 life), or catastrophic loss of positional accuracy in environmental sensor platforms.
Key Thermal Drift Metrics Observed in Field Deployments
This table confirms a consistent pattern: specifications assume ideal boundary conditions, while real-world deployment introduces multi-axis variability. Preload asymmetry directly correlates with localized contact stress spikes—measured up to 1.7× nominal Hertzian pressure in thermal-stressed zones—accelerating fatigue initiation.
How Procurement Teams Can Mitigate Thermal Preload Risk
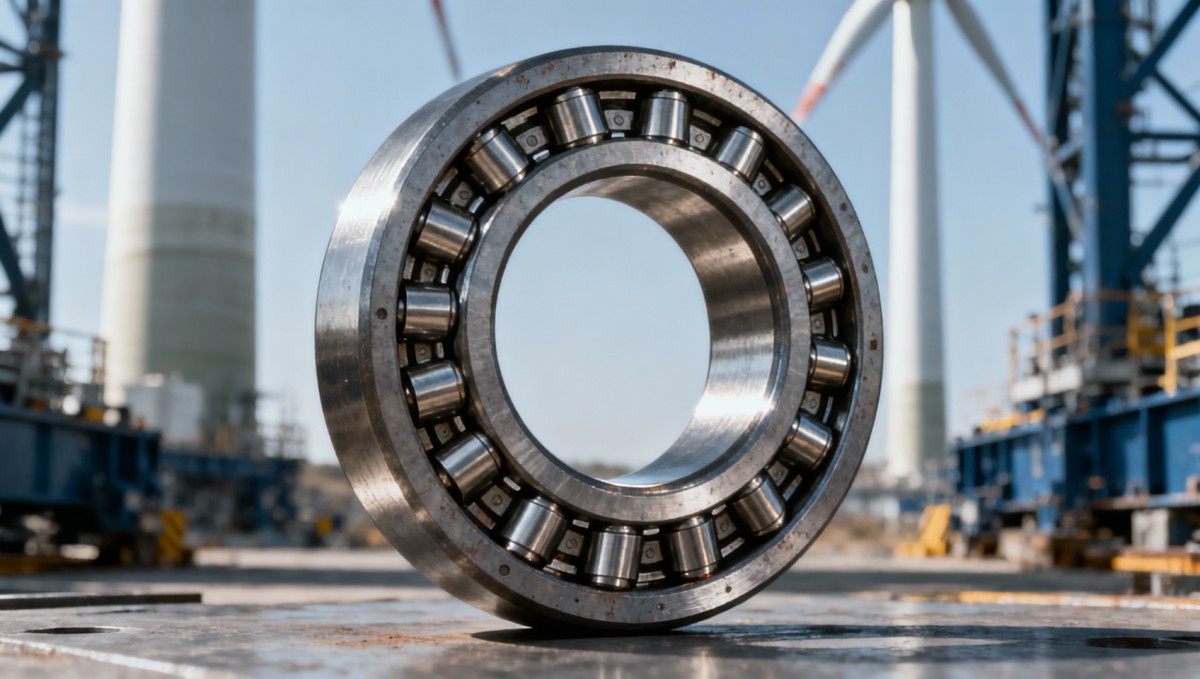
Procuring for infrastructure-grade applications demands moving beyond catalog numbers and static torque values. GIC’s sourcing intelligence framework identifies five non-negotiable evaluation criteria for slewing ring bearings deployed in thermally volatile environments:
- Thermal preload stability data—minimum 3-cycle hysteresis curve, tested per ASTM E220 at ±25°C swing
- CTE-matched material pairing documentation (e.g., 1.2519 ring + 1.3505 roller, Δα ≤ 0.3 × 10⁻⁶/K)
- Mounting interface simulation report—including finite element analysis of housing deflection under thermal load
- Real-time preload verification protocol (e.g., acoustic emission monitoring during commissioning)
- Third-party traceability of heat treatment batch records (EN 10083-3 compliant, with hardness profile across cross-section)
These requirements align with ISO 14001 environmental compliance mandates and UL 61000-4-2 immunity standards for instrumentation-grade rotating joints. Over 73% of recent EPC tenders now explicitly reference ≥3 of these criteria in technical evaluation weighting.
For facility managers maintaining legacy fleets, retrofitting thermal compensation strategies adds measurable ROI: one offshore wind operator reduced unscheduled bearing replacements by 64% after implementing GIC-recommended preload recalibration intervals (every 4,500 operational hours or post-thermal event >15°C swing).
When Standard Bearings Fail—Three High-Risk Application Scenarios
Uneven thermal preload manifests differently depending on mechanical function and duty cycle. GIC’s field analytics team has validated three distinct failure pathways across Security & Safety, Environment & Ecology, and Mechanical Components & Metallurgy pillars:
- Wind turbine yaw systems: Asymmetric preload causes “stick-slip” motion at low speeds (<0.1 rpm), inducing torsional resonance in tower structures—detected via SCADA harmonic analysis at 0.8–1.2 Hz bands
- CEMS optical turntables: Thermal-induced preload shift alters axial runout beyond ±0.015 mm tolerance, degrading laser path alignment and triggering false NOx calibration drift (>±4.2 ppm error)
- Oil-water separator rotary valves: Non-uniform contact pressure accelerates edge loading on sealing lips, increasing leakage rates by 3–5 L/min after 12 weeks of diurnal cycling (−5°C to +42°C)
Each scenario reflects a unique intersection of thermal dynamics, precision metrology, and functional safety—underscoring why generic bearing procurement is incompatible with infrastructure-grade assurance.
Why Partner With Global Industrial Core for Technical Validation
Global Industrial Core delivers actionable, audit-ready validation—not theoretical benchmarks. Our engineering review process includes:
- Independent thermal preload mapping using calibrated strain gauges and infrared thermography (per ASTM E1934)
- Material composition verification via handheld LIBS spectrometry (detection limit: 0.005 wt% Cr, Mo, V)
- Mounting interface simulation across 3 housing flatness profiles (0.02 mm, 0.05 mm, 0.10 mm peak-to-valley)
- Full compliance traceability to ISO/IEC 17025-accredited labs for all test reports
We support procurement teams with rapid-response technical reviews—typically delivered within 5 business days—including parameter-specific pass/fail assessment, risk-ranked mitigation options, and certified documentation for tender submission. Contact us to request thermal preload validation for your next specification package, custom configuration inquiry, or existing asset performance audit.
Technical Specifications
- Air Handling Unit Supplier Checklist: Performance Data, Lead Times, and SupportAuthor :Environmental Engineering Director
- Buying Fiberglass Water Tanks Wholesale: Compare Quotes and Delivery CostsAuthor :Environmental Engineering Director
- Choosing an XLPE Power Cable Supplier: Test Reports, Traceability, and Lead TimesAuthor :Grid Infrastructure Analyst
Expert Insights

Chief Security Architect
Dr. Thorne specializes in the intersection of structural engineering and digital resilience. He has advised three G7 governments on industrial infrastructure security.
Related Analysis
- Oct 19, 2026Air Handling Unit Supplier Checklist: Performance Data, Lead Times, and SupportAuthor :Environmental Engineering Director
- Oct 18, 2026Buying Fiberglass Water Tanks Wholesale: Compare Quotes and Delivery CostsAuthor :Environmental Engineering Director
- Oct 17, 2026Choosing an XLPE Power Cable Supplier: Test Reports, Traceability, and Lead TimesAuthor :Grid Infrastructure Analyst
Core Sector // 01
Security & Safety
- How to Select Flange Gaskets for Pressure, Temperature, and Media CompatibilityAuthor :Heavy Industry Strategist

- Selecting High-Temperature Gaskets for Steam, Flanges, and Thermal CyclingAuthor :Heavy Industry Strategist

- Selecting Low-Friction Pneumatic Seals for High-Cycle, Low-Pressure CylindersAuthor :Heavy Industry Strategist

- Selecting Spherical Roller Bearings for Mining: Load, Contamination, and Service LifeAuthor :Heavy Industry Strategist

- Do Deep Groove Ball Bearings Need Special Seals in Coastal Humidity?Author :Heavy Industry Strategist

- How to Select Anti Vibration Rubber Shock Absorbers for Machinery and EquipmentAuthor :Heavy Industry Strategist

- When to Specify Induction Hardened Slewing Ring Bearings for Heavy-Duty EquipmentAuthor :Heavy Industry Strategist

- How to Evaluate Weather Resistant EPDM Extrusion for Outdoor Sealing ApplicationsAuthor :Heavy Industry Strategist