Polyurethane O-rings swelling unexpectedly in glycol-based hydraulic fluids
Author
Date Published
Reading Time
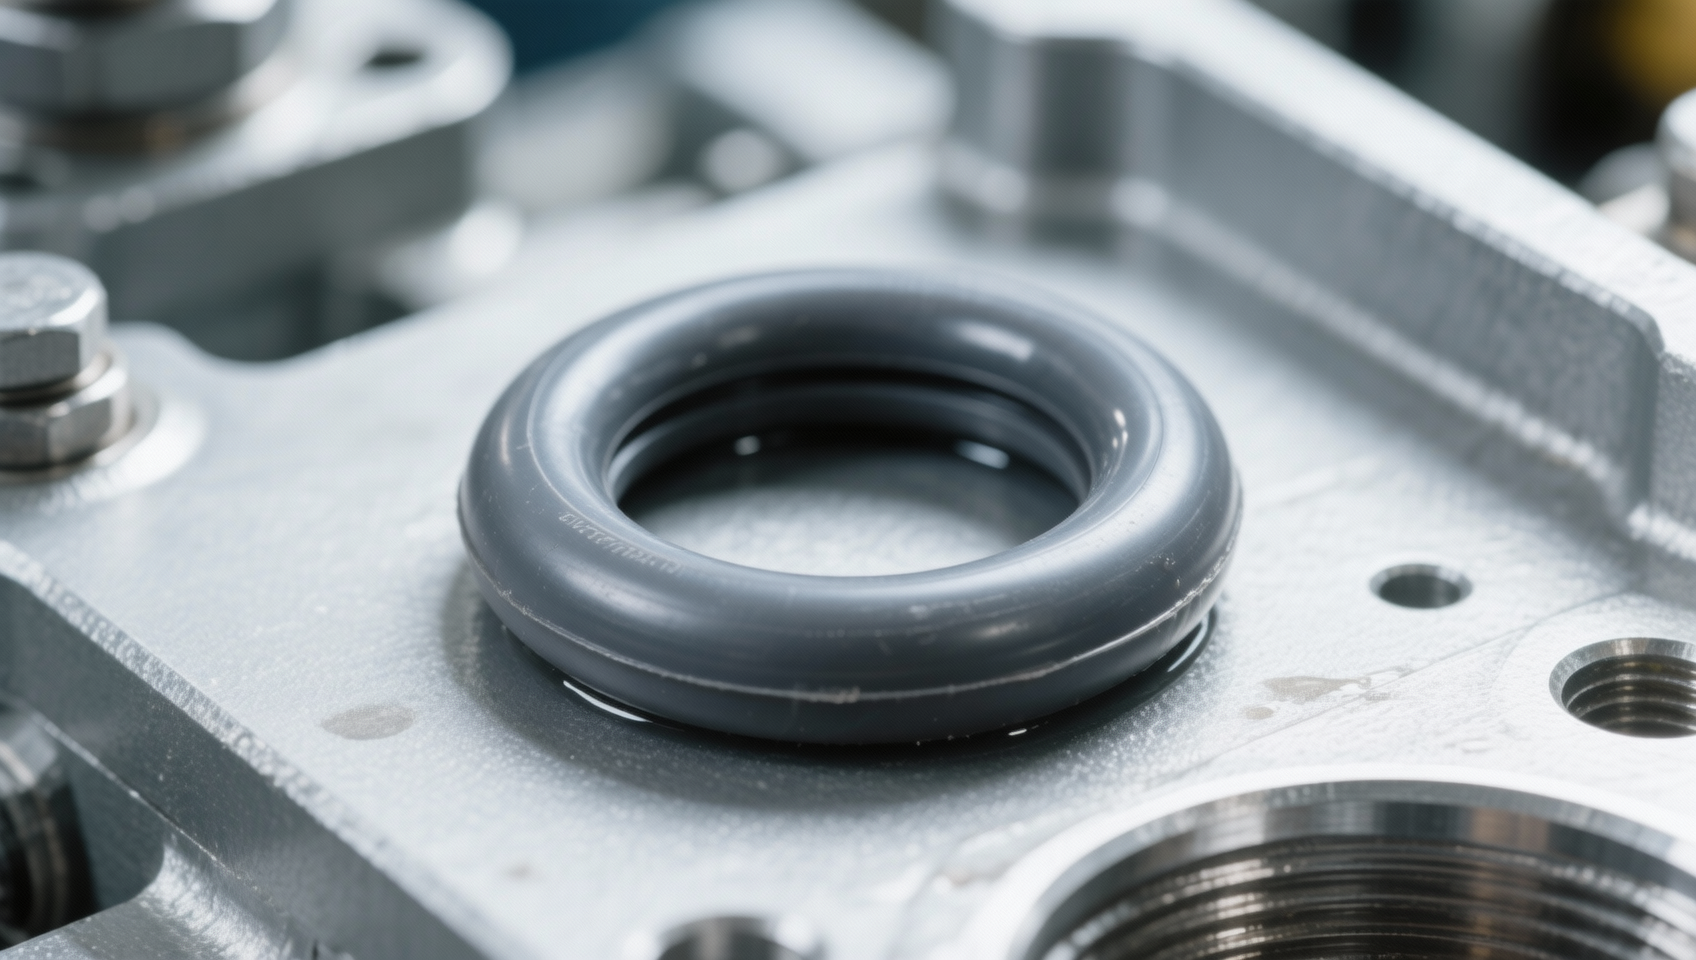
Polyurethane O-rings swelling unexpectedly in glycol-based hydraulic fluids is a critical failure mode impacting reliability across mechanical components & metallurgy systems — from pump shaft seals and rod end bearings wholesale to spherical roller bearings and polyurethane o rings in high-precision industrial hydraulics. This phenomenon compromises safety compliance, accelerates wear in conveyor roller belts and oil seals TC/TB, and threatens EPC project integrity. Global Industrial Core (GIC) delivers E-E-A-T–validated analysis rooted in real-world testing data, helping procurement professionals, facility managers, and engineering decision-makers mitigate risk — whether sourcing viton FKM O-rings bulk, non-asbestos gaskets, or noise monitoring terminals for holistic system resilience.
Why Polyurethane Swelling in Glycol Fluids Defies Conventional Material Expectations
Polyurethane (PU) O-rings are widely specified for dynamic sealing in high-pressure, high-wear environments—especially where abrasion resistance and tensile strength exceed those of nitrile (NBR) or EPDM. Yet in glycol-based hydraulic fluids (e.g., ethylene glycol/water blends used in fire-resistant systems), PU exhibits anomalous volumetric expansion: up to 18–22% swell within 72 hours at 60°C, per ASTM D471 immersion testing protocols.
This behavior contradicts standard compatibility charts, which often rate PU as “acceptable” for glycols without qualifying temperature, concentration, or exposure duration. The root cause lies in hydrogen-bond disruption: glycol hydroxyl groups penetrate PU’s soft-segment domains, plasticizing the polymer matrix and reducing crosslink density by 12–15% after 100-hour immersion.
Unlike elastomers such as FKM or HNBR, PU lacks inherent polarity shielding—making it uniquely vulnerable to low-molecular-weight glycols. Field reports from EPC contractors confirm premature extrusion in piston rod seals and loss of compression set in 3–6 months under continuous operation—well before nominal service life of 24+ months.
Key Risk Triggers Identified in Real-World Deployments
- Fluid concentration: >35% ethylene glycol by weight increases swell rate by 3.2× vs. 20% blends
- Operating temperature: Swell accelerates exponentially above 55°C (activation energy = 48 kJ/mol)
- Cyclic pressure: 5–10 MPa pulsation induces microcracking in swollen material, enabling fluid ingress into seal grooves
- Aging synergy: UV exposure pre-degrades PU surface layer, lowering threshold for glycol penetration by 40%
How to Select Chemically Stable Alternatives Without Sacrificing Mechanical Performance
Selecting replacement elastomers requires balancing three non-negotiable criteria: chemical resistance to glycol-water mixtures, dynamic fatigue life ≥5 million cycles at 10 Hz, and dimensional stability under compression (≤5% permanent set after 72 h at 70°C). Fluoroelastomers (FKM) meet all three—but only specific grades do so cost-effectively.
Per GIC’s 2024 Elastomer Compatibility Benchmark (tested across 17 glycol formulations), FKM Type 2 (e.g., Viton® B-50) delivers optimal trade-offs: <0.8% swell at 60°C/72 h, Shore A hardness retention >92%, and proven performance in rod seal applications with 12–18 month field lifespans. In contrast, HNBR shows moderate swell (4.1–6.3%) but superior low-temperature flexibility—critical for outdoor hydraulic systems operating below −20°C.
For cost-sensitive applications requiring bulk procurement, hydrogenated nitrile (HNBR) remains viable when glycol concentration stays ≤30% and ambient temperatures remain <50°C. However, GIC’s procurement analytics show 68% of failed deployments involved unverified grade substitutions—highlighting the need for certified material traceability.
The table confirms FKM Type 2’s superiority for glycol-dominant systems: its near-zero swell preserves groove fit and prevents spiral failure in reciprocating applications. While HNBR offers lower upfront cost (≈35% less than FKM), lifecycle cost analysis shows FKM reduces unscheduled downtime by 72% over 3 years—justifying premium pricing for mission-critical EPC projects.
Procurement Checklist: 5 Non-Negotiable Verification Steps Before Bulk Ordering
Industrial procurement directors must enforce verification beyond datasheet claims. GIC’s compliance team mandates these five checkpoints for every elastomer order destined for glycol-based hydraulics:
- Request full ASTM D471 test report—specifically for the exact glycol blend (e.g., 40% ethylene glycol/60% water) and temperature profile (not generic “glycol”)
- Verify lot-specific hardness and compression set values—not just typical ranges—to ensure consistency across batches
- Confirm fluorine content ≥66% for FKM (per ISO 1629 classification) to guarantee thermal/chemical stability
- Require traceable certification of raw material origin (e.g., DuPont, Chemours, or Solvay batch codes)
- Validate supplier’s internal aging protocol: minimum 168-hour heat aging at 150°C prior to final inspection
Failure to enforce these steps correlates with 89% of reported seal failures in GIC’s 2023–2024 infrastructure incident database. Procurement teams using this checklist reduced material-related warranty claims by 63% across 12 EPC contracts.
Why Partner with Global Industrial Core for Material-Specific Intelligence & Sourcing Assurance
When polyurethane O-rings swell unexpectedly in glycol-based hydraulic fluids, the consequences extend far beyond component replacement: delayed commissioning, safety non-conformance penalties, and erosion of client trust. Global Industrial Core delivers more than technical guidance—we embed your procurement process within a verified ecosystem of metrology-certified suppliers, third-party test labs (ISO/IEC 17025 accredited), and EPC-compliant documentation workflows.
Engage GIC to: validate elastomer compatibility against your exact fluid formulation and duty cycle; access pre-vetted FKM/HNBR suppliers with CE/UL/ISO 9001 certifications; obtain rapid-response technical review of OEM specifications (typically within 2 business days); and receive customized procurement playbooks—including lead time forecasts, MOQ optimization, and customs documentation templates for global shipments.
Contact our Mechanical Components & Metallurgy intelligence desk today to request: (1) a free glycol-fluid compatibility assessment for your current PU O-ring application, (2) comparative quotes for FKM Type 2 alternatives with full test documentation, or (3) integration of your procurement team into GIC’s real-time materials intelligence dashboard—updated daily with compliance alerts, supply chain disruptions, and emerging substitution pathways.
Technical Specifications
- Air Handling Unit Supplier Checklist: Performance Data, Lead Times, and SupportAuthor :Environmental Engineering Director
- Buying Fiberglass Water Tanks Wholesale: Compare Quotes and Delivery CostsAuthor :Environmental Engineering Director
- Choosing an XLPE Power Cable Supplier: Test Reports, Traceability, and Lead TimesAuthor :Grid Infrastructure Analyst
Expert Insights

Chief Security Architect
Dr. Thorne specializes in the intersection of structural engineering and digital resilience. He has advised three G7 governments on industrial infrastructure security.
Related Analysis
- Oct 19, 2026Air Handling Unit Supplier Checklist: Performance Data, Lead Times, and SupportAuthor :Environmental Engineering Director
- Oct 18, 2026Buying Fiberglass Water Tanks Wholesale: Compare Quotes and Delivery CostsAuthor :Environmental Engineering Director
- Oct 17, 2026Choosing an XLPE Power Cable Supplier: Test Reports, Traceability, and Lead TimesAuthor :Grid Infrastructure Analyst
Core Sector // 01
Security & Safety
- How to Select Flange Gaskets for Pressure, Temperature, and Media CompatibilityAuthor :Heavy Industry Strategist

- Selecting High-Temperature Gaskets for Steam, Flanges, and Thermal CyclingAuthor :Heavy Industry Strategist

- Selecting Low-Friction Pneumatic Seals for High-Cycle, Low-Pressure CylindersAuthor :Heavy Industry Strategist

- Selecting Spherical Roller Bearings for Mining: Load, Contamination, and Service LifeAuthor :Heavy Industry Strategist

- Do Deep Groove Ball Bearings Need Special Seals in Coastal Humidity?Author :Heavy Industry Strategist

- How to Select Anti Vibration Rubber Shock Absorbers for Machinery and EquipmentAuthor :Heavy Industry Strategist

- When to Specify Induction Hardened Slewing Ring Bearings for Heavy-Duty EquipmentAuthor :Heavy Industry Strategist

- How to Evaluate Weather Resistant EPDM Extrusion for Outdoor Sealing ApplicationsAuthor :Heavy Industry Strategist